Dubbed as the “highway over the sea”, the Incheon Bridge is the longest bridge in Korea
Incheon Bridge
Dubbed as the “highway over the sea”, the Incheon Bridge is the longest bridge in Korea.
Rebar Splicing Methods
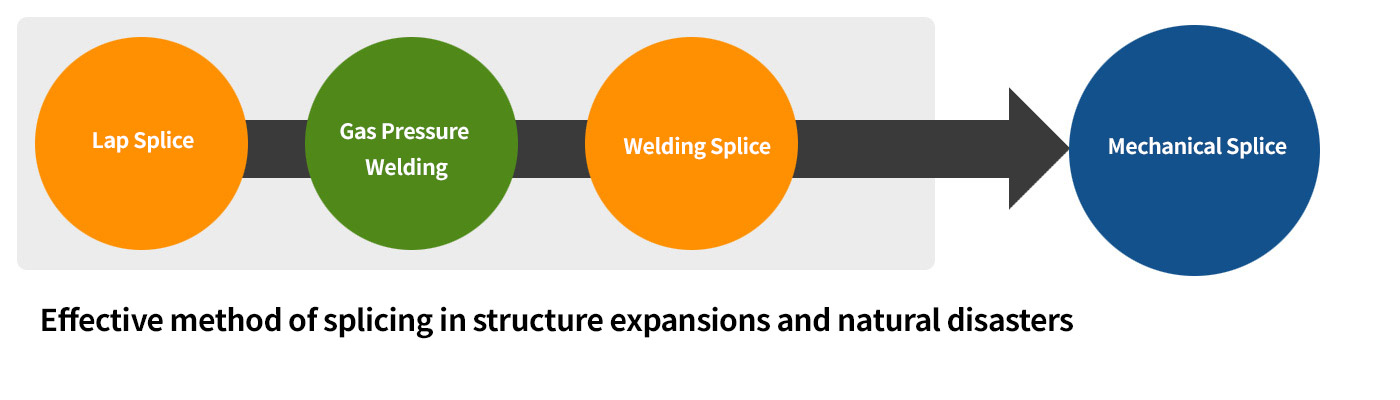
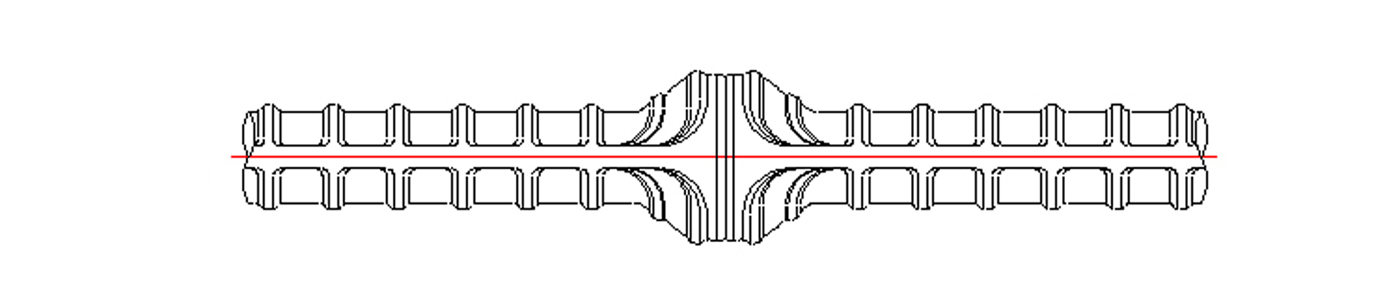
Rebar splicing methods fall into four main categories: lap splicing, gas pressure welding, welded splicing, and mechanical splicing.
As structures grow larger and resilience to natural hazards becomes more critical, mechanical coupling has emerged as the most effective splicing method, widely proven for its structural performance and constructability.
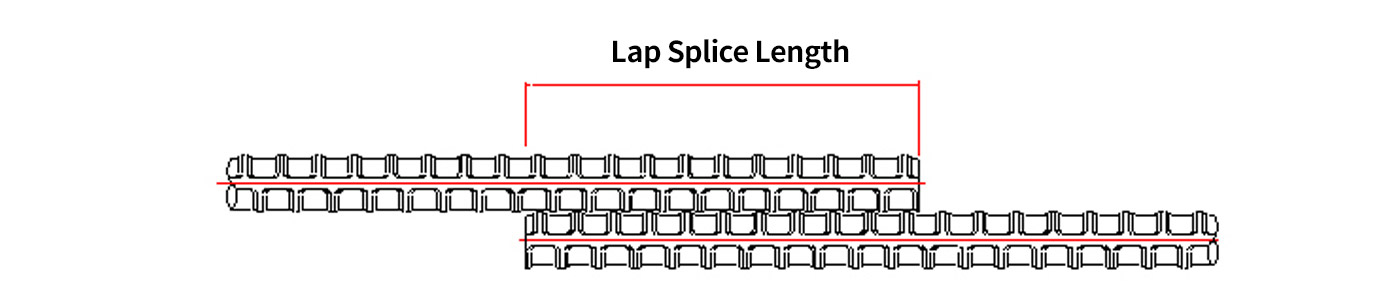
Rebar lap splicing is a traditional method widely used for its simplicity and cost-effectiveness. However, increasing structural scale and seismic design requirements have led to severe rebar congestion and constructability issues, resulting in growing regulatory restrictions on its application. Specifically, lap splicing presents constructability challenges when attempting to comply with RC code limitations regarding splice locations. Furthermore, bond-splitting cracks at concrete member joints can trigger sudden brittle failure and rapid loss of load capacity. Therefore, to prevent bond-splitting failure, designing lap splices requires strict selection of splice locations, lap lengths, concrete cover, and bar spacing.
Rebar lap splicing is a traditional method widely used for its simplicity and cost-effectiveness. However, increasing structural scale and seismic design requirements have led to severe rebar congestion and constructability issues, resulting in growing regulatory restrictions on its application.
Specifically, lap splicing presents constructability challenges when attempting to comply with RC code limitations regarding splice locations. Furthermore, bond-splitting cracks at concrete member joints can trigger sudden brittle failure and rapid loss of load capacity. Therefore, to prevent bond-splitting failure, designing lap splices requires strict selection of splice locations, lap lengths, concrete cover, and bar spacing.
Originally adapted in Japan from U.S. rail track joining techniques, gas pressure welding includes both manual and automated processes.
Developed from American railway joint technology, this process was adapted for rebar connections in Japan and is not currently utilized for reinforcement in the United States.
The process aligns two rebar ends, heating them to roughly 1300°C using an oxy-acetylene flame. Pressure is applied while the metal remains solid, bonding the interface through solid-state atomic diffusion.
To apply gas pressure welding, mating surfaces must be ground flat prior to processing, as surface irregularities prevent proper bond formation at the interface.
High localized heating creates a Heat-Affected Zone (HAZ), requiring verification against cold-working principles outlined in governing design codes (e.g., KCS Concrete Specifications, ACI 318/318R, Chapter 7, Section 3).
High-strength rebar (SD400+), in particular, contains elevated carbon and manganese content, risking localized embrittlement after welding. For Tempcore-processed rebar, heat application degrades structural strength, demanding rigorous quality management.
Rebar welded splicing is a method of joining rebar by melting it with a heat source. This method consists of a fusion zone, where the rebar ends and the welding rod melt and combine, and a heat-affected zone (HAZ), where the surrounding rebar is altered yet not melted by the welding heat.
Because high welding temperatures induce oxidation, failing to take proper precautions burns off essential trace elements (such as carbon and manganese), leading to significant losses in tensile strength and toughness.
Field-applied welding poses additional challenges due to reduced joint reliability and electrical hazards, complicating on-site safety and quality control
다운로드 정보 입력
다운로드 전에 아래 정보를 입력해 주세요.
GLOBAL NO.1 in the specialized mechanical rebar splice with a competitive advantage in technology and a creative passion
Head Office : 02-549-0675 Chungju Plant : 043-856-6640~2